Applications
Manufacturers of non-standard precision parts
Ultrasonic

CNC Machining for Core Ultrasonic Equipment Precision Components
CNC machining for core ultrasonic equipment precision components is a new-generation hybrid precision manufacturing process that combines traditional CNC precision cutting with ultrasonic high-frequency vibration. It delivers high-precision, damage-free core parts for various ultrasonic equipment including ultrasonic welding machines, ultrasonic cleaning instruments, ultrasonic medical devices and ultrasonic detection instruments. It fundamentally guarantees the vibration transmission efficiency, energy output stability and long-term operation reliability of ultrasonic equipment, serving as the key manufacturing segment in the modern high-end ultrasonic equipment industry chain that overcomes the processing challenges of hard-to-machine brittle materials.
Core Machining Categories & Application Scenarios
Ultrasonic CNC machining covers a full range of high-demand functional components, with typical categories as follows:
- Ultrasonic Transducer Parts: Horns, vibrator bases and energy conversion metal blocks, which ensure efficient and accurate transmission of ultrasonic vibration energy without energy loss.
- Ultrasonic Welding Equipment Parts: Balancing nuts for 15K/20K/35K welding machines, welding head mounting bases and aluminum alloy amplitude modulators, which guarantee vibration coaxiality and pressure stability during the welding process.
- Ultrasonic Medical Device Parts: Ceramic vibration heads for ultrasonic scalpels, titanium alloy working tips for ultrasonic dental scalers and ceramic bases for ultrasonic imaging probes, which meet the biocompatibility and high-precision vibration requirements in medical scenarios.
- Ultrasonic Industrial Equipment Parts: Vibrator mounting plates for ultrasonic cleaners, wear-resistant ceramic probes for ultrasonic detectors and core cavities for ultrasonic flow sensors, which ensure long-term wear-resistant operation in industrial scenarios.
The machining accuracy of these parts directly determines the final performance of ultrasonic equipment. According to general industry standards, the linear tolerance of core parts is controlled within ±0.005~±0.01mm, the surface roughness of critical vibration mating surfaces is Ra ≤ 0.2μm, and the flatness of vibration transmission contact surfaces is ≤0.003mm. This completely eliminates micro-cracks and energy loss caused by stress concentration, enabling ultrasonic equipment to achieve a vibration energy transmission efficiency of over 95%.
Exclusive Process Control Tailored for Ultrasonic Scenarios
Targeting the core requirements of ultrasonic parts — zero internal stress, high vibration transmission efficiency and zero damage for hard brittle materials — the industry has established an exclusive full-process control system:
- Precise Material Adaptation: Leveraging the unique flexible cutting principle of high-frequency vibration, we can efficiently process hard brittle materials that are difficult to machine with traditional processes, including industrial ceramics, sapphire, quartz crystal and silicon carbide. It also adapts to various ductile materials such as titanium alloy, aluminum alloy and special composite materials, fully covering the material requirements for all categories of ultrasonic equipment parts.
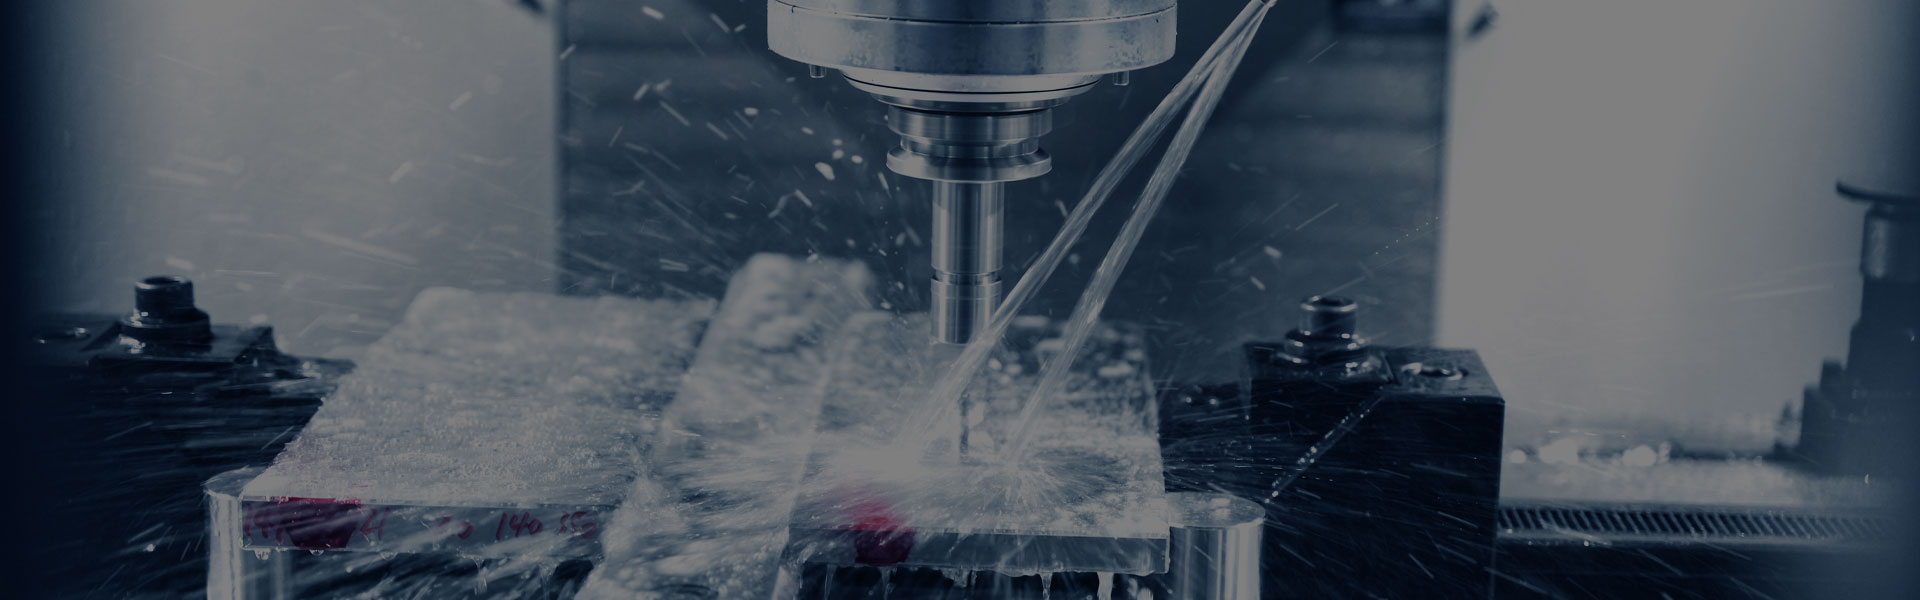
- Hybrid Precision Forming Machining: Special CNC machining centers integrated with ultrasonic high-frequency micro-vibration are adopted. While rotating for cutting, the tool is superimposed with micron-level axial vibration to gently peel off materials through pulsed impact. Complex special-shaped curved surfaces, ultra-fine deep holes and thin-wall lightweight structures can be fully machined in a single setup, fundamentally avoiding common industry defects such as edge chipping, cracking and micro-damage of hard brittle materials.
- Stress-Free Post-Treatment Processes: After machining, exclusive stress-relief annealing and ultra-precision mirror polishing processes are performed to completely eliminate the residual surface stress generated during machining, ensuring no structural deformation or fatigue fracture risk for parts under long-term high-frequency vibration operation.
- Full-Dimensional Vibration Performance Inspection: High-precision coordinate measuring machines (CMM), surface roughness testers and ultrasonic impedance analyzers are used for 100% full inspection on the geometric tolerances, surface precision and vibration transmission performance of parts. Each batch of parts is delivered with complete vibration performance inspection reports.
Core Technical Advantages
- Zero Damage for Hard Brittle Material Machining: It completely solves the pain points of edge chipping, micro-cracks and internal damage that are extremely common in traditional machining processes for hard brittle materials such as ceramics and sapphire. The finished product yield of parts is greatly increased to over 98%, ensuring the structural integrity of ultrasonic parts during long-term high-frequency vibration operation.
- Full-Process Cost & Efficiency Optimization: High-frequency vibration-assisted cutting drastically reduces tool friction resistance, extending tool service life by 3 to 5 times. Meanwhile, the traditional multi-process machining is simplified to complete all procedures in a single setup, eliminating the need for multiple subsequent polishing and repairs. The overall machining efficiency is improved by over 40%, drastically shortening the production cycle.
- Outstanding Complex Structure Forming Capability: Leveraging the precise positioning of CNC systems and the flexible vibration cutting characteristics, we easily realize one-time forming of ultra-thin wall structures, high-difficulty deep micro-holes and multi-curve complex shapes, fully releasing the structural design space of ultrasonic equipment and helping the iterative upgrading of product performance.
Related Products
Service Hotline:
Contact
Phone:+86 13622624429 (same as whatsapp)
Email: croesus.lo@xjcmachiningparts.com
Address:No. 8, Haibin Road, Wusha, Chang'an Town, Dongguan, Guangdong, China
QR code
Scan to Visit Our Website


Support: baten.cc
 QR code
 +86 13622624429
 croesus.lo
 croesus.lo@xjcmachiningparts.com
 +86 13622624429